 GST No.27DSUPK8009N1ZT


 Our Products

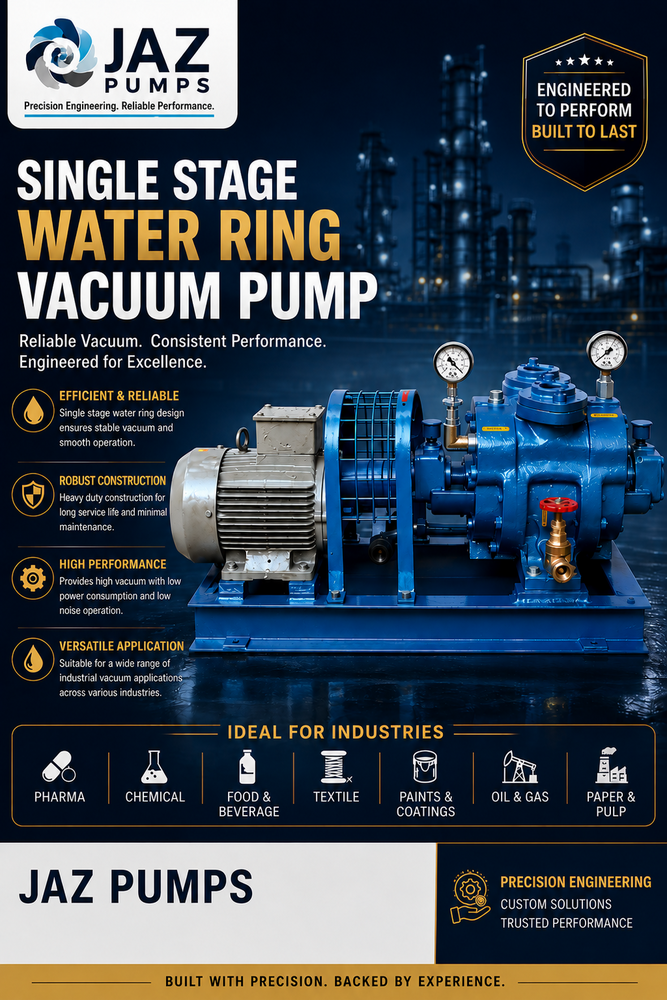
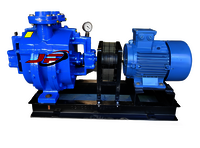
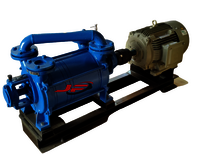
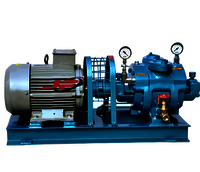
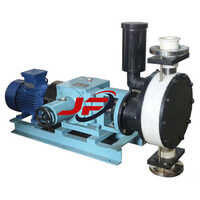
Water Ring Vacuum Pump
28500 INR/Set
Minimum Order Quantity : 1 Sets
Working Temperature Up to 80C
Voltage 415V/380V/230V (as per model/design)
Usage Industrial Vacuum Applications, Industrial Vacuum Applications
Theory Liquid Ring
Suction Type Single Stage
Structure Monoblock/Coupled
Standard As per international vacuum standards
Speed 1440 rpm / 2900 rpm (depends on design)
Seals Type Mechanical Seal/Gland Packing
Pump Type Water Ring Vacuum Pump
Priming Self-priming
Pressure Negative Pressure (Vacuum generation)
Power 1 HP to 100 HP (as per model)
Noise Level Low Noise Operation
Mounting Type Baseplate/Skid Mounted
Max Suction Up to 710 mmHg (Approx. 94% vacuum)
Material Cast Iron / Stainless Steel / Other Alloys
Inlet/Outlet Flange (as per capacity)
Head Size Not Applicable (Vacuum Pump)
Fuel Type Electric Drive
Fuel Tank Capacity Not Applicable (Electric)
Frequency 50 Hz / 60 Hz
Flow Rate 100 to 22000 LPH (varies by model)
Features Consistent Performance, Efficient & Reliable, Rugged Construction, Low Maintenance, Engineered for Excellence
Discharge Pressure Atmospheric Discharge
Control System Manual/Automatic
Capacity Model specific (up to 22000 LPH)
Caliber 50mm to 200mm (model dependent)
Application Pharmaceutical, Chemical, Beverage, Textile, Food, Paper, Oil, Cement, and General Industries, Pharmaceutical, Chemical, Beverage, Textile, Food, Paper, Oil, Cement, and General Industries
About this product
-
A single-stage water ring vacuum pump (also known as a single-stage liquid ring vacuum pump) is a positive-displacement machine that uses an eccentrically mounted impeller and a rotating water ring to pull a continuous, non-pulsating vacuum in a single compression phase.Distillation, filtration, paper dewatering, condenser air extraction, vacuum priming, and chemical/pharmaceutical drying processes.
Versatility and Application Range
This water ring vacuum pump is suitable for a broad array of industrial sectors, including pharmaceuticals, chemicals, beverages, textiles, food processing, and general industries. Designed to handle a variety of service mediums compatible with its construction materials, it is appropriate for applications with wet gases and vapors, delivering reliable vacuum performance even under demanding environments.
Robust Construction for Durability
Engineered for longevity, the pump boasts a corrosion-resistant paint finish, cast iron or stainless steel options, and can be tailored with different sealing systems. Its IP55-rated motor, dynamic balancing for low vibration, and monoblock or coupled structure provide minimal maintenance requirements and reliable operation both indoors and outdoors.
Efficiency and Performance Highlights
Equipped with features like self-priming, minimal vibration, and low noise, this vacuum pump offers consistent performance and operational efficiency. With capacities up to 22,000 LPH and vacuum generation up to approximately 94%, it supports various installation and control configurations, with spare parts readily available for uninterrupted industrial processes.
FAQ's of Water Ring Vacuum Pump:
Q: How does the water ring vacuum pump handle wet gases and vapors?
A: The pump uses the liquid ring principle, creating a rotating liquid seal that enables it to effectively handle and extract wet gases and vapors, making it suitable for moisture-rich industrial processes.Q: What installation environments are suitable for this vacuum pump?
A: This pump is engineered for both indoor and outdoor installations. Its corrosion-resistant construction and IP55 motor protection ensure dependable operation in diverse environments, including areas with exposure to moisture or contaminants.Q: When should the pump be used in industrial applications?
A: It is ideal for use whenever efficient vacuum generation is required, especially in sectors like pharmaceuticals, chemicals, food processing, textiles, and paper manufacturing where handling of wet gases or vapors is common.Q: Where can the vacuum pump be mounted or installed?
A: The pump supports mounting on either a baseplate or skid, and connections are available in both threaded and flanged options as per model size, allowing flexible installation in most industrial settings.Q: What maintenance and spare parts availability can be expected?
A: Designed for durability and low maintenance, this pump has dynamically balanced components that reduce wear. Spare parts are readily available, ensuring uninterrupted operation and easy servicing.Q: How does the pump ensure operational efficiency and safety?
A: The pump meets ISO and CE safety standards, features a TEFC or flameproof motor (available upon request), and provides options for manual or automatic control, offering both efficiency and compliance with international safety norms.Q: What are the main benefits of using this water ring vacuum pump in industrial processes?
A: Key benefits include high operational durability, consistent vacuum performance, efficient handling of moisture-laden gases, low noise and vibration, and the flexibility to meet varied industry needs with minimal maintenance and robust safety compliance.Explore Additional Categories




Contact Us